
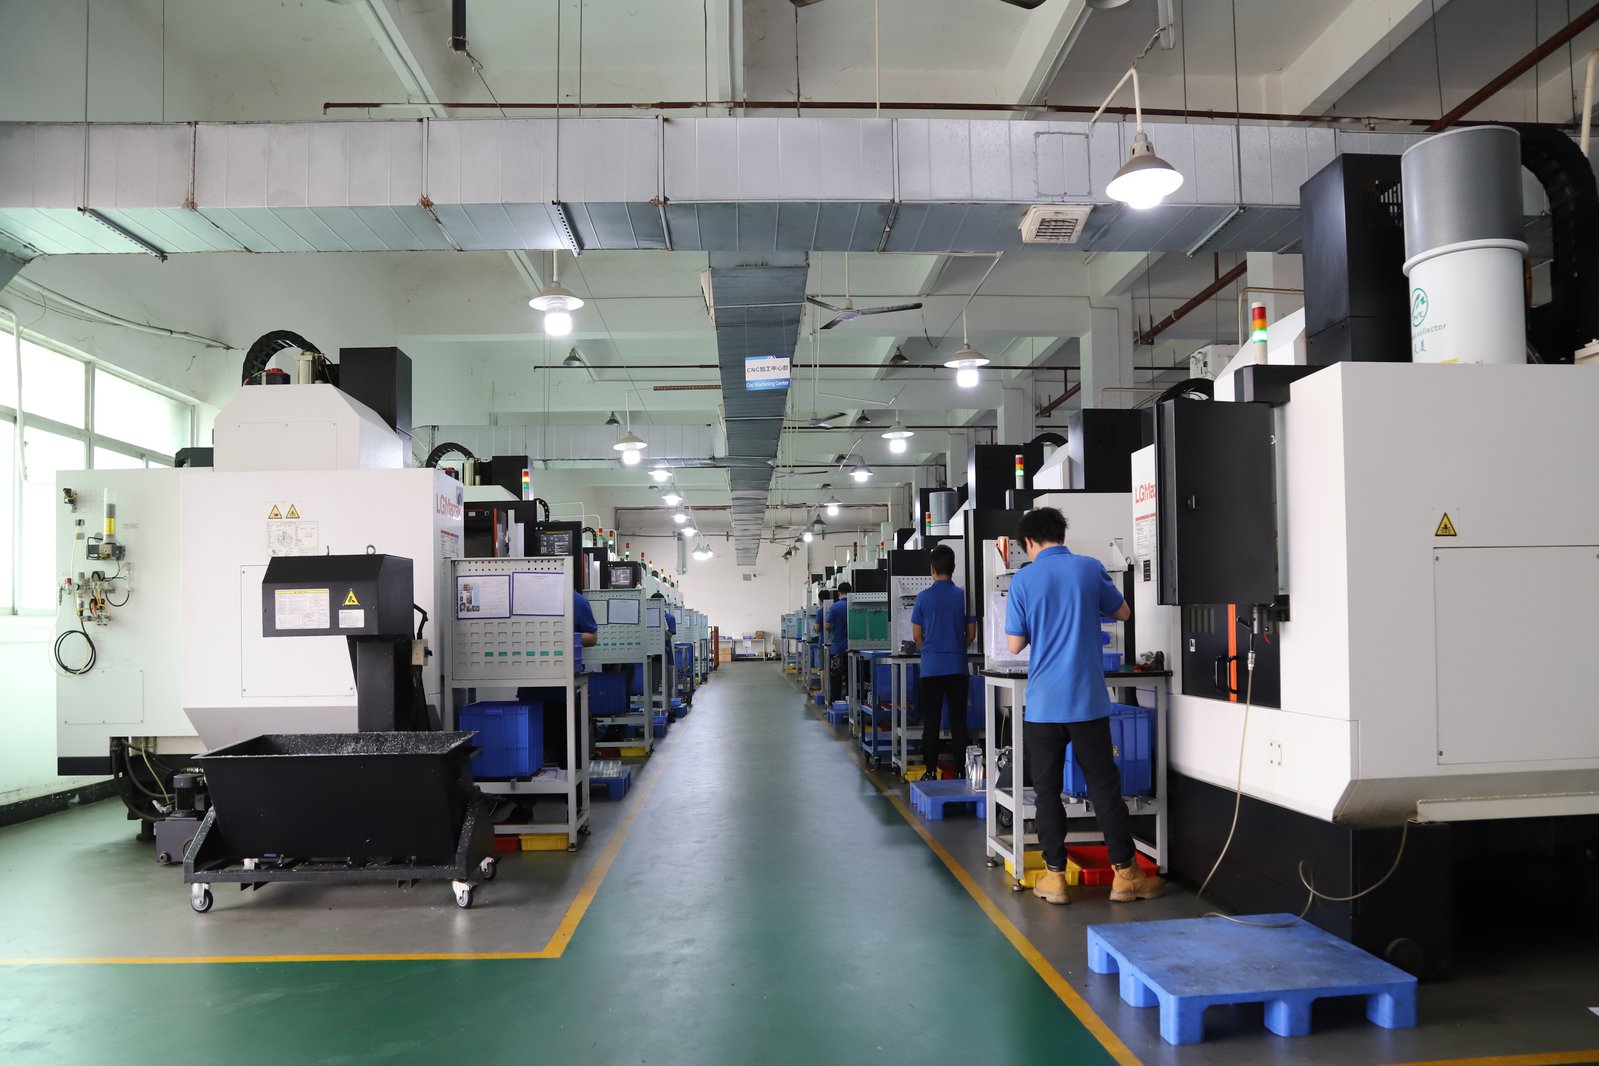
Every precision machining quote carries a number nobody asks about until it matters: what tolerance can the supplier actually hold, and what surface finish will the part really ship with? The practical answer from a controlled China precision machining shop is steady. Milled and turned features hold ±0.003 mm, precision-ground surfaces reach ±0.002 mm, and process capability on key characteristics is reported at Ppk ≥ 1.67 initial. Surface finish follows a similar ladder, from a standard machined Ra 1.6 µm down to a ground Ra 0.2–0.4 µm. The discipline is not in the headline numbers; it is in knowing where to spend them on the drawing, how each callout changes the price, and how the result is verified when the parts are a hemisphere away.
- Tolerance envelope: ±0.003 mm milled and turned features, ±0.002 mm precision-ground surfaces, Ppk ≥ 1.67 at the initial study on key characteristics and Cpk ≥ 1.33 on general characteristics. Capability is reported per characteristic: every report names the feature, its tolerance band, the sample size, the sigma method, and the study window.
- Finish ladder: Ra 1.6 µm standard machining, Ra 0.8 µm controlled pass, Ra 0.2–0.4 µm grinding.
- Where to spend: tight bands on mating, sealing, and datum features only; general tolerance elsewhere.
- Verification: CMM against the drawing datum reference frame, profilometer for finish, instruments identified on the report.
What tolerance can a China precision machining supplier realistically hold?
A controlled China precision machining shop works inside a production envelope that is narrower than buyers fear and wider than suppliers boast. Milled and turned features hold ±0.003 mm when the process is set up for them — the machine is capable, the tooling is appropriate, and inspection is matched to the drawing. Precision-ground surfaces that seat, seal, or define a datum move to ±0.002 mm, which is a different process class with its own cost and measurement requirements.
The acceptance criterion is not the tolerance band alone; it is capability. A supplier that holds ±0.003 mm occasionally is different from one whose process runs at Ppk ≥ 1.67 at the initial study on the key characteristics, because capability predicts the whole lot while a single measured part proves only itself. Ask for capability data on the features that carry function, and treat the first-article report as the start of the evidence rather than the end of it.
Be equally clear about what is not realistic. ±0.001 mm on every dimension of a large aluminum plate is not a production tolerance; it is a laboratory condition that collapses under temperature and fixturing. A serious supplier flags over-toleranced drawings in the technical review, naming which features are difficult to hold at your quantity and why. That response is a feature, not a weakness — it means the quote is built on process knowledge rather than on optimism.
Where do the tight tolerances belong on a drawing?
Tolerance is a budget, and it should be spent where the part spends it. Features that mate a part to another component, seat a bearing or a seal, or carry the datum structure an assembly builds on justify the tight band. A cosmetic pocket, a clearance hole, or a non-functional profile does not — it runs at the general tolerance and stays cheap.
The pattern that drives cost up fastest is scatter. Drawings that tighten every dimension because it costs nothing on paper push every feature into slower machining and extra inspection, and the price rises across the board without improving the part. The same drawing with the general tolerance stated and three or four functional features tightened will quote lower and hold the function that matters, because the shop can machine the bulk of the part in one stable setup.
State the general tolerance standard on the drawing so there is no argument later. Buyers commonly reference ISO 2768 or the shop's standard ±0.1 mm for untoleranced dimensions, with the functional features called out individually. When the general tolerance is written down, the quote, the machining, and the inspection all read the same default, and the supplier can flag the features that genuinely need the tight band rather than guessing which ones you care about.
What surface finish is realistic on a precision-machined part?
Surface finish on machined parts follows a repeatable ladder, and each rung costs more than the one above it. A standard milling or turning pass lands around Ra 1.6 µm — acceptable for most structural and cosmetic surfaces. Where a part slides, seals, or carries a controlled appearance, a deliberate finishing pass reaches Ra 0.8 µm. Precision-ground faces that seat against another component or run in a bearing move to Ra 0.2–0.4 µm, which is a ground finish, not a machined one.
Name the process with the Ra value, because the number alone leaves the how ambiguous. Ra 0.8 µm can be reached by a fine machining pass, by lapping, or by polishing — each with different cost, cycle time, and effect on the geometry. Add the direction of lay where it matters: a seal face or a bearing surface behaves differently depending on whether the finish runs with or across the motion. A complete callout names the value, the process, and the lay, and that is what a shop can quote honestly.
Watch the finish spec creep past the function. A drawing that calls Ra 0.4 µm on a face nobody touches pays for grinding time and inspection on a feature that could run at Ra 1.6 µm, and the money shows up in the quote. Let the surface finish follow the function — sealing, sliding, bearing, or appearance — and reserve the fine finishes for the faces that earn them.
How much do tight tolerances and fine finishes actually cost?
Tolerance and finish do not carry a fixed percentage; they carry process consequences. A feature tightened from ±0.1 mm to ±0.05 mm costs little, because the same machine and the same measurement routine handle it. Tightened to ±0.003 mm, the same feature may demand a slower feed, a dedicated tool, temperature control, and a CMM program — a different cost class entirely. The jump is not linear, and it differs per feature, per material, and per quantity.
Finish behaves the same way. Moving from Ra 1.6 µm to Ra 0.8 µm is usually a finishing pass; moving to Ra 0.2–0.4 µm adds a grinding operation, separate setup, and its own inspection. The way to price this honestly is a drawing review, where the supplier returns the features that drive cost and the reasons. A review that says "this bore is the cost driver, here is why, and here is what loosening it saves" is worth more than any rule of thumb.
The material decides how far the envelope stretches. Aluminum holds the tight bands easily and cuts predictably; stainless and titanium cut harder, wear tools faster, and carry more drift in long runs; plastics move with temperature, moisture, and fixture pressure. A quote that names the same tolerance for every material is a quote that has not thought about your material. The material selection guide on this site walks the trade-offs between the two dominant families and what each one does to your tolerance budget.
Why do geometric callouts deserve their own care on the drawing?
Size tolerances describe how big a feature is; geometric tolerances describe how it sits in space. A bore can measure perfectly to its ±0.003 mm size callout and still be positioned wrong relative to the datum structure, or lean instead of standing square. For a precision-machined part that mates into an assembly, position, flatness, parallelism, and concentricity usually matter more than the size bands, and they are the callouts that separate a part from a part that works.
Geometric tolerances demand a measurement method. A position tolerance is verified against the datum reference frame on a CMM, not with a caliper, and the datum structure on the drawing has to be machinable and measurable. Ask how the supplier will measure position and form on your features during the technical review, because a drawing that cannot be measured is a drawing that cannot be held.
Keep the datum structure simple. Every datum adds fixturing and measurement complexity, and a drawing with five datums on a part that needs two is paying for discipline it does not use. Define the features that matter — the faces the assembly locates from — and let the rest of the geometry follow. When the datum structure is clean, the supplier can hold the tolerances and prove it, and the inspection report reads back against the same frame you designed.
How should critical tolerances and finishes be verified?
A tolerance claim is only as strong as the measurement behind it, and on a China-sourced part the measurement method should be agreed before the order, not discovered at first article. Size and position on critical features are measured against the drawing datum reference frame — typically a CMM, with the instrument, its calibration date, and the measurement settings named on the report. Surface finish is read with a profilometer over the specified area, in the specified direction.
Ask what the report will contain and judge it against your drawing. Does it map every critical feature to the datum reference frame, or does it list convenient bench readings? Does it identify the instrument that produced the numbers, and is that instrument on a calibration cycle? A report that names its instruments and their calibration status is a report you can trust; a block of numbers with no source is a claim without a witness.
Understand measurement uncertainty on the tight features. A CMM reading carries its own error, and when the tolerance band is thin, the difference between the reported value and the true value starts to consume the allowance. A supplier that can discuss that margin is measuring seriously, and its process capability number — Ppk ≥ 1.67 at the initial study on key characteristics and Cpk ≥ 1.33 on general characteristics. Capability is reported per characteristic: every report names the feature, its tolerance band, the sample size, the sigma method, and the study window. — is what converts a measured sample into a prediction about the lot. The quality page on this site lists the CMM, surface, and vision instruments behind our reports and how the data links to each lot.
How do tolerances and finishes interact with secondary operations?
Machining is rarely the last thing that touches a surface. Anodizing grows a coating that changes dimensions; plating adds thickness; passivation changes the surface chemistry without changing the geometry much; bead blasting roughens a finish you may have just measured. Every secondary operation has to be sequenced against the tolerance and finish callouts, and the drawing should say which order the operations run in.
Decide which surfaces are finished before the coating and which after. A bore that must stay at ±0.003 mm after anodize has to be machined with the coating thickness in mind, or masked, or reamed after coating — each with a different cost and a different risk. The same logic applies to grinding before plating on a seal face. When the drawing names the finishing sequence, the supplier can quote the real process instead of discovering it at first article.
Put the secondary operations on the quote explicitly, because they are where finishes drift. A part that looks identical before and after anodize can change dimension by enough to break a tight fit, and a polishing pass can round the very edge the drawing needed sharp. The discipline is to name every operation, verify the result after the last step, and measure the critical features in the state the part ships in, not the state it left the machine in.
What belongs in the RFQ to make quotes comparable?
Most quote comparison fails because the quotes are not comparing the same thing. Two suppliers can quote the same drawing with different general tolerances, different finish assumptions, and different included operations, and the prices will differ for reasons that have nothing to do with capability. The fix is an RFQ that removes the ambiguity before the quotes arrive.
Send a toleranced 2D drawing with the datum structure, feature control frames, and finish callouts; the material grade and condition; the quantity and any planned growth; the general tolerance standard you intend to apply; and the surface finish expectation on the functional faces. Add the documentation you want — a first-article report, material certificate, capability data on key characteristics — because a quote that includes the paperwork is priced differently from one that does not.
Then read the differences deliberately. A supplier that returns a technical review naming the cost-driving features, the verification method, and a realistic delivery has engaged with your part; a supplier that returns a single number has not. Compare the reviews as much as the prices, and use the envelope in this guide — ±0.003 mm milling, ±0.002 mm grinding, Ppk ≥ 1.67 initial, and the finish ladder — as the yardstick for what a controlled China precision machining shop should state without hedging.
Frequently Asked Questions
What tolerance can a China precision machining supplier realistically hold?
Milled and turned features hold ±0.003 mm in a controlled process, and precision-ground surfaces reach ±0.002 mm. Capability at Ppk ≥ 1.67 at the initial study on key characteristics and Cpk ≥ 1.33 on general characteristics. Capability is reported per characteristic: every report names the feature, its tolerance band, the sample size, the sigma method, and the study window is the acceptance criterion that matters, because it predicts the whole lot rather than one measured part.
Where should the tight tolerances go on a drawing?
Only where function earns them: mating diameters, bearing seats, seal faces, and the datum structure an assembly builds on. Cosmetic pockets and non-functional profiles should run at the general tolerance, because scatter of tight callouts multiplies cost and inspection time without improving the part.
What surface finish is realistic on a machined part from China?
Standard milled faces finish around Ra 1.6 µm, a controlled machining pass reaches Ra 0.8 µm, and precision grinding gets to Ra 0.2–0.4 µm. Name the process and the direction of lay with the Ra value, because a bare Ra number leaves the how open to interpretation.
How much do tight tolerances and fine finishes add to the price?
Each tightening step adds inspection time, slower machining, and more scrap risk rather than a fixed percentage. A feature tightened from ±0.05 mm to ±0.003 mm can move a part into a different process and measurement class, so the honest answer comes from a drawing review, not a rule of thumb.
How should a critical tolerance be verified on a China-sourced part?
Measured against the drawing datum reference frame with a calibrated instrument — typically a CMM for GD&T callouts and a profilometer for surface finish — and reported with the instrument identified. Hand checks against a scratched edge prove nothing on a ±0.003 mm feature.
How do tolerances and finishes interact with the material?
Every material holds its own envelope: aluminum is stable and easy to cut, stainless and titanium are harder and carry more tool-wear drift, and plastics move with temperature and moisture. The supplier's tolerance claim should be quoted per material and feature, not as one universal number.
What should I put in the RFQ to make quotes comparable?
A toleranced 2D drawing with datums and finish callouts, the material grade and condition, the general tolerance standard you intend to apply, the quantity, and the surface finish you expect on functional faces. Suppliers then quote the same scope, and the differences between quotes become readable.
Want a quote that names the tolerance and the finish honestly?
Send the part file with your toleranced 2D drawing and material spec, and ask for a technical review that flags the cost-driving features before you commit. Contact the China Precision Machining team to start the drawing review.